
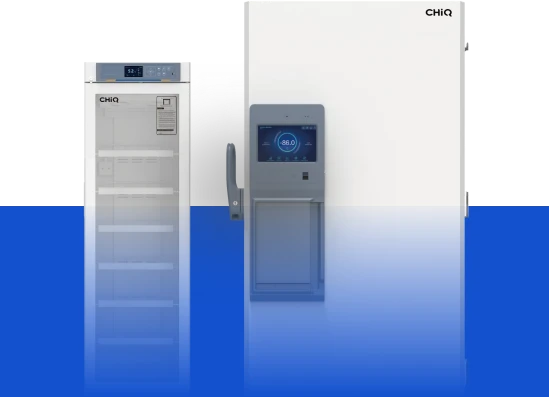
CHIQ, a core subsidiary of Changhong Group—China’s leading home appliance and technology conglomerate—has been dedicated to the research, design, manufacturing, and global distribution of cryogenic and biomedical storage solutions since its founding in 2002. Leveraging Changhong Group’s deep-rooted manufacturing legacy and cutting-edge innovation platform (established in 1958 and headquartered in Mianyang, Sichuan), CHIQ integrates advanced refrigeration technologies with the evolving needs of the life sciences. This synergy has enabled the company to develop a diverse, high-performance product portfolio that meets the demanding requirements of biomedical laboratories, research institutions, healthcare providers, and public health systems worldwide.
-

Years of Cryogenic Technology
40
+ -

R&D Center
5,000
m² -

Manufacturing Plant
85,000
m² -

Patents
500
+
Capital Market Recognition
A major milestone in the company's growth came in 2022 with its successful listing on the Beijing Stock Exchange (BSE). This achievement established CHIQ as the first BSE-listed company in Anhui Province, while also setting a record for speed: the listing process was completed in just 111 days, with review approval granted within only 37 days. These milestones reflect the company's operational excellence, robust governance, and strong market confidence.
Company Strength
Our Core Capabilities, Proven and Trusted
-

Innovation Strength
Driven by innovation, CHIQ has built a world-class R&D team over the past two decades, boasting nearly 500 proprietary scientific innovations including invention patents and utility model patents. Its flagship technology, New Mixed Working Medium Throttling Refrigeration Technology and Its Application, has won the Second Prize of National Technical Invention and the First Prize from the China Refrigeration Society, cementing the company’s leading position in refrigeration science and engineering.
Adhering to user-centric innovation, CHIQ provides customized intelligent solutions for diverse sectors: biobanks & sample storage, blood safety & vaccine preservation, pharmaceutical cold chain, IoT-enabled LN2 storage systems, as well as secure storage for laboratories and research facilities. Engineered for safety, reliability and environmental sustainability, CHIQ products are widely adopted by hospitals, CDCs, academic institutions, public health authorities, research laboratories, genetic engineering centers and animal health organizations worldwide. -

Global Footprint
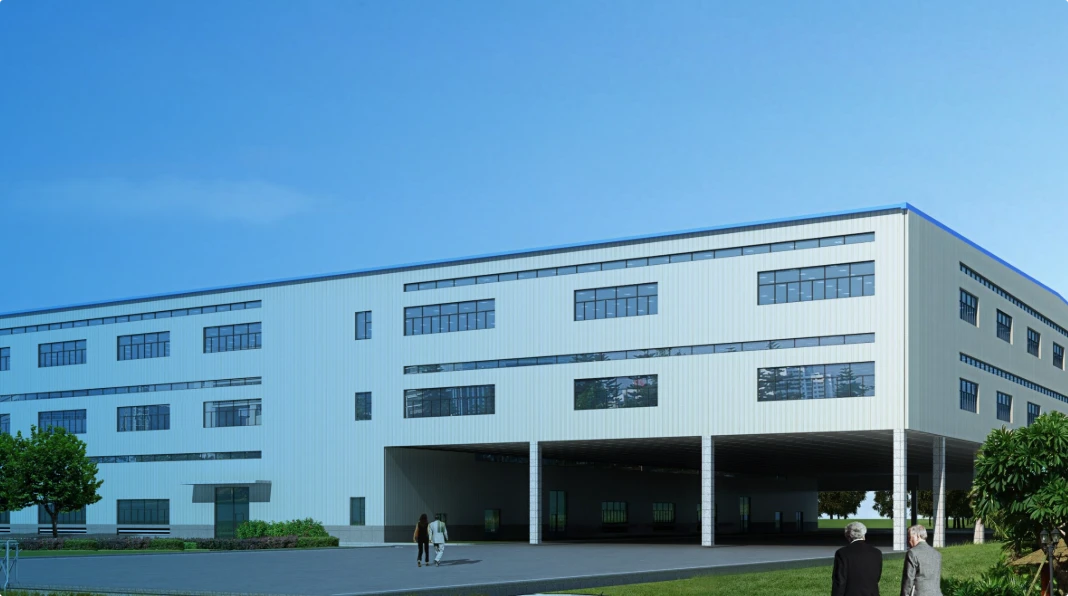
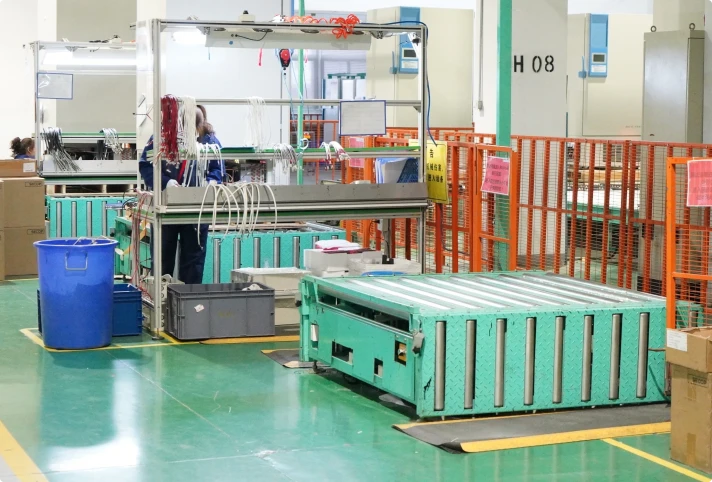
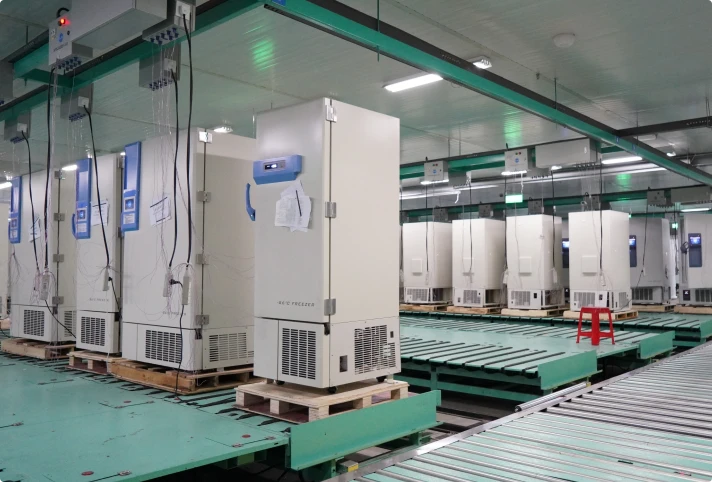
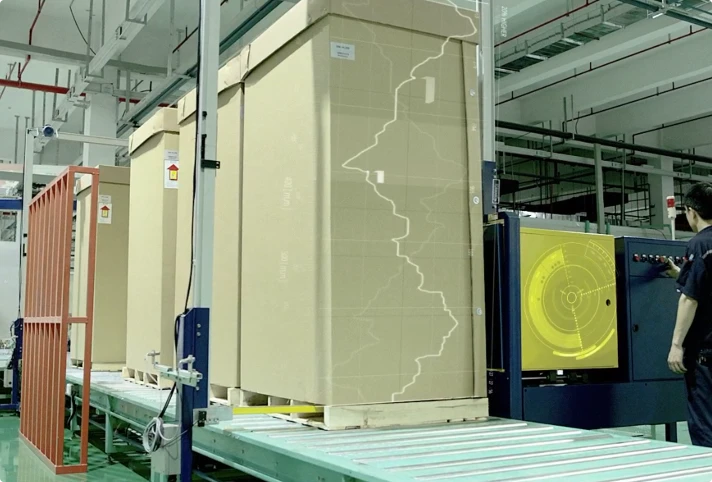
CHIQ owns more than 5,000 m² of R&D space and over 85,000 m² of manufacturing and testing premises, equipped with fully automated low-temperature equipment production lines, type laboratories and a complete testing & pilot workshop. Backed by a full-service global support network and international certifications, CHIQ products are exported to more than 100 countries across Europe, the Americas, Asia-Pacific, the Middle East and Africa.
Driven by innovation, CHIQ has built a world-class R&D team over the past two decades, boasting nearly 500 proprietary scientific innovations including invention patents and utility model patents. Its flagship technology, New Mixed Working Medium Throttling Refrigeration Technology and Its Application, has won the Second Prize of National Technical Invention and the First Prize from the China Refrigeration Society, cementing the company’s leading position in refrigeration science and engineering.
Adhering to user-centric innovation, CHIQ provides customized intelligent solutions for diverse sectors: biobanks & sample storage, blood safety & vaccine preservation, pharmaceutical cold chain, IoT-enabled LN2 storage systems, as well as secure storage for laboratories and research facilities. Engineered for safety, reliability and environmental sustainability, CHIQ products are widely adopted by hospitals, CDCs, academic institutions, public health authorities, research laboratories, genetic engineering centers and animal health organizations worldwide.
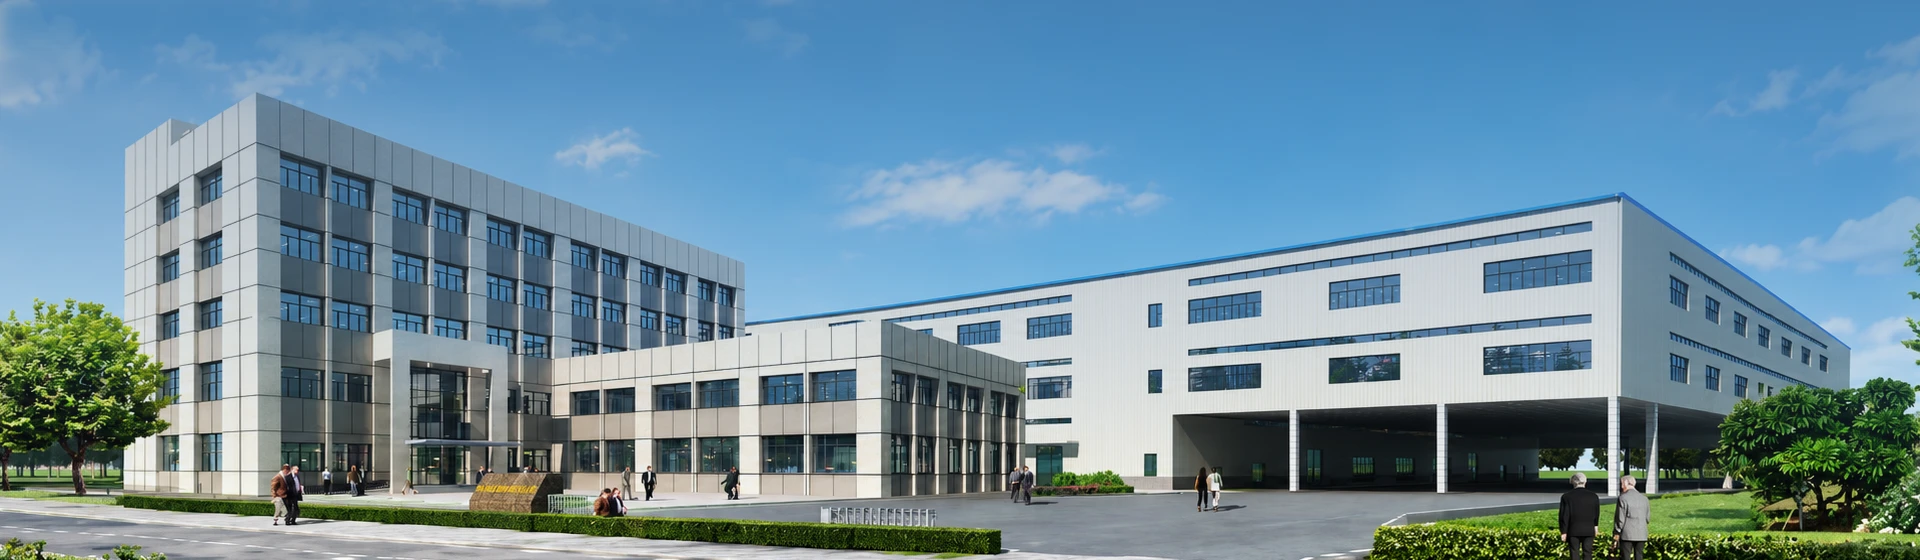
CHIQ owns more than 5,000 m² of R&D space and over 85,000 m² of manufacturing and testing premises, equipped with fully automated low-temperature equipment production lines, type laboratories and a complete testing & pilot workshop. Backed by a full-service global support network and international certifications, CHIQ products are exported to more than 100 countries across Europe, the Americas, Asia-Pacific, the Middle East and Africa.
Looking Ahead
CHIQ remains firmly committed to continuous product innovation, expansion of category offerings, and sustainable development. With a strategic focus on green technologies, energy-efficient designs, and diversified global trade models, the company aims to make a lasting contribution to human health and environmental protection.
CHIQ – “Preserving Life with Advanced Science”.
We are committed to becoming the global leader in customized biomedical system solutions.
Honors & Qualifications
Certified Excellence, Verified Credentials — Explore Our Officially Recognized Qualifications and Industry Accreditations
- Patents
- Product
- Company
-
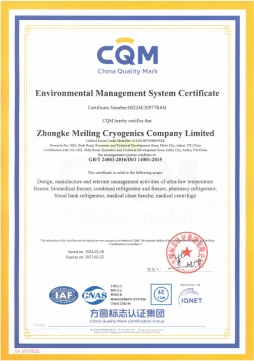
ISO-14001-CQM
-
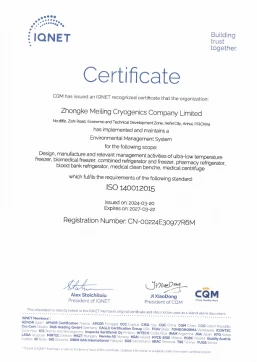
ISO-14001-IQNET
-
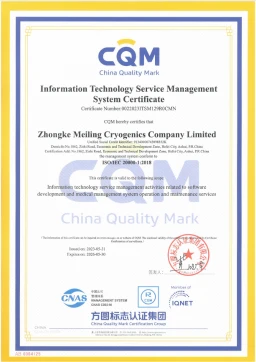
ISO-20000-CQM
-
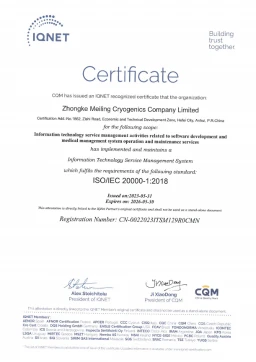
ISO-20000-IQNET
-
ISO-14001-CQM
-
ISO-20000-CQM
-
ISO-14001-IQNET
-
ISO-20000-IQNET
-
ISO-14001-IQNET
-
ISO-20000-IQNET
-
ISO-14001-CQM
-
ISO-20000-CQM
Company Environment
A realistic showcase of the company, production facilities, and workshop environment
Brands We Serve
Professional Service / Sincere Attitude / Premium Quality / High Efficiency